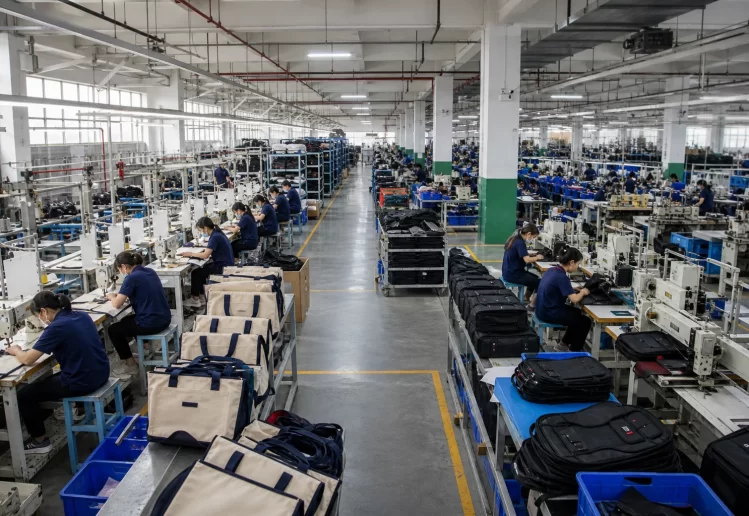
Can One Factory Manage a Whole Bag Range, or Do You Need Several?
A buyer building a range faces this question once and then lives with the answer for years. One factory that handles everything is simpler to manage; several factories that each excel at something usually produce a better range.
The right answer depends less on factory capability than on what the range actually contains. A range of four totes in similar constructions is a different problem from a range that spans totes, backpacks, crossbody bags and small leather goods. The first consolidates well; the second rarely does.
Consolidation has real advantages that are easy to undervalue. One relationship, one set of payment terms, one quality standard, one shipment to consolidate, and one conversation when something goes wrong. Those advantages compound over time and are worth paying something for.
Specialisation has advantages that are easy to overstate until a problem appears. A factory that builds backpacks every day understands reinforcement, load paths and strap geometry in a way a tote factory does not. Buying a backpack from a tote factory is not impossible; it is simply buying a first attempt.
This article sets out what a range actually is once you break it into production families, when a single factory is the better answer, when several are unavoidable, how to split a range without creating management overhead, what consolidation really saves, and how to move from several vendors to fewer without losing quality.
- What a Range Really Contains
- When One Factory Is the Right Answer
- When Several Factories Are Unavoidable
- Reading Capability, Not Catalogue
- How to Split a Range Sensibly
- What Consolidation Really Saves
- The Hidden Costs of a Single Source
- Keeping Quality Consistent Across Vendors
- Capacity, Seasonality and Risk
- Sampling a Range With One or Many
- Contracts, Tooling and Terms
- Moving From Several to Fewer
- Lead Factory Plus Specialists
- Where the Structure Shows Up in Cost
- Building a Risk Register
- A Decision Framework
- FAQ
What a Range Really Contains
Before deciding on factories, a buyer needs to see the range as production families rather than as products.
Why product names mislead
Sellers describe a bag by what it is for; factories describe it by how it is built. A “weekender”, a “commuter bag” and a “gym tote” may be the same construction problem under three marketing names.
Reading the range as a factory would read it is the first step toward a sensible sourcing decision.
Group by construction, not by name
A tote and a shoulder bag with the same construction, same material and similar panel count belong to one family. A tote with a structured base and a soft tote with a single seam do not.
Grouping by construction reveals that ranges that look diverse on a catalogue page are often two or three production problems.
The families that usually appear
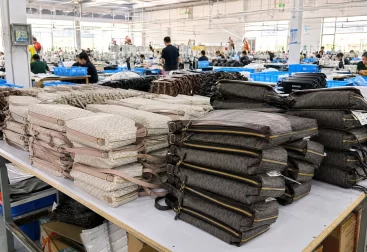
Most bag ranges resolve into soft non-structured bags, structured bags with reinforcement, backpacks with load-bearing systems, small leather goods, and technical or insulated pieces.
Each family carries distinct machinery, distinct operator skill and distinct quality risks.
Panel count as a proxy
Panel count is a rough but useful measure of complexity. A bag with six panels and one with twenty-four are not comparable in labour or in failure modes.
Ranges that span very low and very high panel counts rarely consolidate well into one line.
| Family | Core skill | Typical machinery | Quality risk |
|---|---|---|---|
| Soft unstructured | Drape and clean seaming | Lockstitch, skiving | Edge finish, sagging |
| Structured | Reinforcement and shape | Post-bed, heat press | Distortion, board delamination |
| Backpacks | Load paths and strap geometry | Heavy-duty machines, bar tack | Anchor failure, comfort |
| Small leather goods | Precision and edge work | Fine needles, edge paint | Alignment, edge cracking |
| Technical or insulated | Sealing and barrier integrity | Seam sealing, welding | Leak paths, cold bridging |
| Hardware-heavy | Fitting installation | Presses, setting tools | Pull-out, finish damage |
How many families are you actually buying
Most mid-sized ranges contain two or three real families. That number, not the product count, determines whether one factory is realistic.
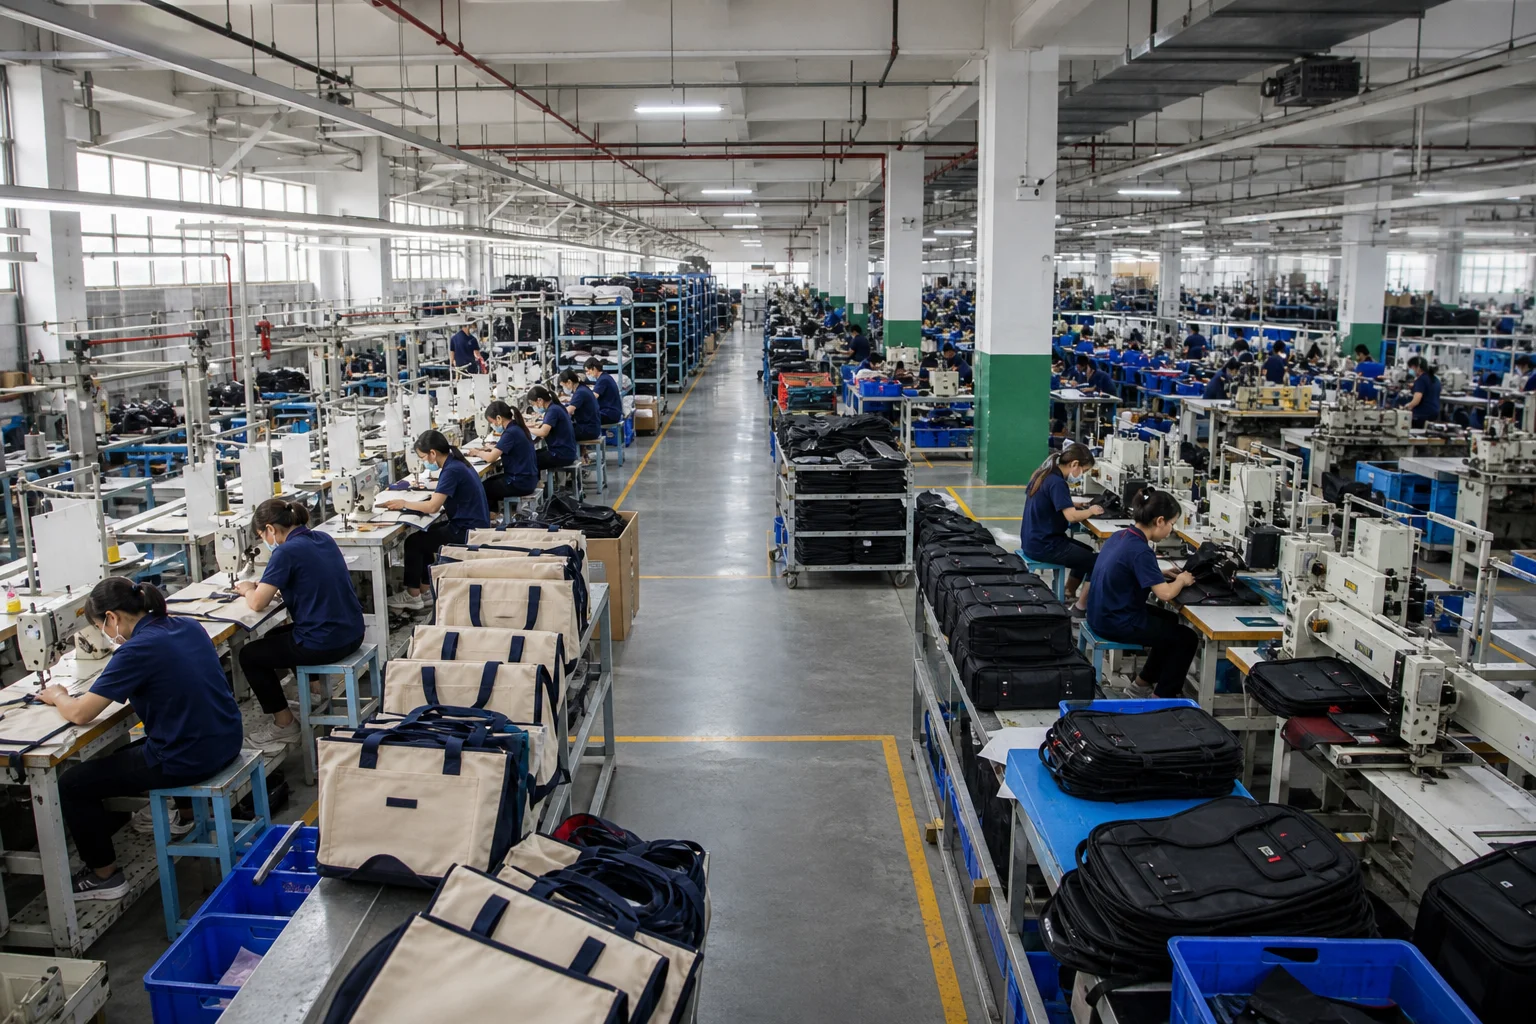
When One Factory Is the Right Answer
A single factory works well under conditions that are specific and testable.
The range sits in one family
If every product shares construction logic and material, one factory loses nothing by building all of it. This is the strongest case for consolidation.
Volume per style is meaningful
One factory needs enough volume per style to justify setup. Consolidating five styles at low volume each may produce worse economics than three styles at higher volume.
Material is shared
Shared material means shared purchasing, shared colour consistency and shared waste. A range built from three PU qualities across one factory is easier to control than the same range split three ways.
You are early in the relationship
With a new factory, one relationship is easier to test than three. Consolidation lets you learn how a partner behaves before spreading risk.
Consolidation is not a discount strategy. It is a management-capacity strategy, and it pays when your own attention is the scarce resource.
What to verify before consolidating
Consolidation should follow evidence, not optimism. Ask for the construction closest to your hardest product, not your easiest, and inspect that sample closely.
When Several Factories Are Unavoidable
Some ranges cannot be served well by one factory, and pretending otherwise creates predictable failures.
Construction families diverge sharply
Where a range spans soft totes and load-bearing backpacks, the machinery and operator skill differ enough that one factory will be strong in one and weak in the other.
Material systems differ
Coated fabric, PU leather, heavy canvas and insulated laminates require different handling, different needles and different finishing. A factory tooled for one will improvise on the others.
Compliance regimes differ
Where some products require specific testing or documentation and others do not, a specialist often handles the regulated items better than a generalist.
Capacity exceeds one plant
A range that peaks above a single factory’s monthly capacity needs a second source regardless of preference. Discovering this during peak season is expensive.
| Situation | Single factory viable | Better to split |
|---|---|---|
| One construction family | Yes | No need |
| Two to three families | Only with proven breadth | Usually |
| Soft plus technical | Rarely | Yes |
| Peak exceeds capacity | No | Yes |
| Single market, simple range | Yes | Not required |
| Multiple regulated markets | Rarely | Often |
Proving breadth honestly
A factory claiming to cover everything should be able to show output, equipment and samples in each family. Where evidence is thin, treat the claim as an intention rather than a capability.
The cost of forcing it
A factory asked to build outside its competence will accept the order and learn on your product. The learning cost appears as delay, rework and a first shipment that does not match the sample.
Reading Capability, Not Catalogue
Catalogues show what a factory wants to sell. Capability is what it does repeatedly.
Ask for the production mix
What percentage of last year’s output was in the family you need? A factory that built two hundred backpacks among ten thousand totes is not a backpack factory.
Look at the constraint equipment
Bar tackers, post-bed machines, heat presses, seam sealers. Equipment reveals which families a factory genuinely serves, because nobody buys a post-bed machine for occasional work.
Inspect the hardest sample, not the best
Ask for the construction closest to your most difficult product. Factories present their best work by default; the useful question is what happens at the edge of their competence.
Ask who else they build for
A factory already producing in your family for other buyers has solved the problems you are about to encounter. That experience is worth more than a price difference.
| Signal | Reliable indicator | Misleading indicator |
|---|---|---|
| Production mix | Share of output in your family | Catalogue breadth |
| Equipment | Constraint machines present | Machine count |
| Samples | Hardest construction offered | Best construction offered |
| Client base | Similar products in production | Famous brand names |
| Operators | Skill concentrated in family | Total headcount |
| Problem history | Known failure modes discussed openly | Claims of no defects |
Questions that reveal a specialist
A specialist answers technical questions specifically: which reinforcement at the anchor, which needle for the material, where the seam is likely to fail. A generalist answers in generalities.
How to Split a Range Sensibly
Splitting a range badly creates more work than keeping it whole. The split should follow construction lines, not convenience.
Split along family boundaries
Give each factory a coherent family rather than scattered styles. Coherence lets a factory optimise setup, material purchasing and operator assignment.
Scattered allocation forces every factory to hold material for styles it rarely builds.
Keep one family with one factory
Two factories building the same family means two interpretations of the same specification and two sets of quality variation. That is a management cost with no offsetting benefit.
Designate a lead factory
Where several factories serve one range, name one as the reference for shared components, colour standards and packaging. This keeps cross-vendor consistency anchored.
Watch the shared component problem
Zips, hardware and lining used across families must match exactly. Cross-vendor sourcing of the same component is one of the most common causes of visible inconsistency in a range.
What Consolidation Really Saves
Consolidation savings are usually overstated on price and understated on administration.
What the price saving actually is
Volume consolidation produces a modest unit price improvement, and it flattens quickly. The larger effect is usually on setup and tooling amortisation rather than on the unit rate itself.
The administrative saving
One vendor means one set of payment terms, one shipping schedule, one inspection protocol and one relationship. For a small buying team, this is often the dominant benefit.
The quality consistency benefit
One factory applying one standard produces a more coherent range. Colour, stitch density and edge finish vary less when they come from one line.
The freight benefit
Consolidated shipments reduce freight cost and customs complexity. Several vendors means several shipment timings and several sets of documents.
| Benefit | Typical size | Notes |
|---|---|---|
| Unit price | Modest | Flattens quickly with volume |
| Setup amortisation | Meaningful | Larger effect than unit price |
| Administration | Large for small teams | One terms, one schedule |
| Quality consistency | Meaningful | One standard applied once |
| Freight and documents | Meaningful | Fewer shipments, fewer errors |
| Problem resolution | Large | One conversation, clear owner |
What it does not save
Consolidation does not reduce the cost of a factory that cannot build the product. Buying everything from one source because it is simpler can be more expensive than managing two.
The Hidden Costs of a Single Source
Consolidation carries risks that only appear under stress, which is why they are easy to defer indefinitely.
Priority inversion
A single vendor with several customers will allocate scarce capacity somewhere. Without an alternative, the buyer has limited means to influence where.
Even a small secondary source changes the conversation, because the option exists.
Concentration risk
One factory means one fire, one labour dispute, one collapsed bank, one regulatory inspection away from a total supply interruption. Buyers rarely price this risk until they experience it.
Negotiating position
A vendor supplying the entire range knows it. Over time, pricing discipline weakens because the buyer has no credible alternative and both sides know the switching cost.
Innovation stagnation
A single vendor has no competitive pressure to improve construction, suggest material alternatives or invest in new capability. The relationship settles into routine.
Quality drift without comparison
Without a second reference point, gradual deterioration is invisible. Standards slip in ways that are obvious only when compared against another vendor’s interpretation.
| Risk | How it appears | Mitigation |
|---|---|---|
| Concentration | Sudden total interruption | Qualified backup source |
| Negotiating position | Creeping price increases | Periodic market benchmarking |
| Stagnation | No new proposals | Sample challenges, new briefs |
| Quality drift | Standards relax unnoticed | Retained reference samples |
| Capacity squeeze | Your orders deprioritised | Written capacity commitments |
| Knowledge lock-in | Tooling and specs held by them | Own the tooling and files |
The qualified backup
A backup source does not need volume. It needs to have passed sampling and to hold your specifications, so that a switch is a scheduling decision rather than a development project.
Keeping Quality Consistent Across Vendors
Where several factories serve one range, consistency becomes an active management task rather than an assumption.
One specification, written once
The specification must be vendor-neutral and complete: material, construction, stitch density, thread, hardware, tolerances and pack. Any ambiguity will be resolved differently by each vendor.
One approved sample set
Sign off a reference sample per style and keep identical sets with each vendor. Without a physical reference, disputes become arguments about memory.
One inspection protocol
The same sample size, acceptance limits and defect definitions must apply everywhere. Otherwise the vendor with the stricter inspector appears worse.
Shared component sourcing
Where possible, buy or nominate shared components centrally: the same zip, the same hardware, the same lining. Colour and finish variation between suppliers is immediately visible in a range.
| Control | Prevents | Practical action |
|---|---|---|
| Single specification | Different interpretations | Written, measurable, vendor-neutral |
| Reference samples | Memory-based disputes | Signed sets held by each vendor |
| Uniform inspection | False comparisons | One protocol, calibrated inspectors |
| Central components | Visible mismatch | Nominate supplier and shade |
| Shared packaging spec | Carton and label drift | One packaging document |
| Common colour standard | Batch-to-batch drift | Physical standards, not codes alone |
The colour problem
Colour is the most visible inconsistency across vendors. Digital codes are a starting point; physical standards under defined lighting are the only reliable control.
Capacity, Seasonality and Risk
Capacity is the constraint that most often forces a multi-vendor structure, usually later than it should.
Peak versus average
A factory sized for your average month cannot serve your peak. The question is whether the peak can be levelled through planning or must be spread across sources.
Capacity commitments in writing
Verbal assurances about capacity evaporate when a larger customer arrives. Written monthly capacity commitments, with consequences, are worth more than a factory’s floor space.
Seasonal overlap
Factories serving several buyers with the same season face simultaneous peaks. Your peak is not their only peak, and priority is usually commercial rather than contractual.
Geographic concentration
Several factories in one region share labour markets, power supply and logistics. Spreading vendors geographically reduces correlated risk at the cost of management complexity.
| Capacity question | What to ask | Red flag |
|---|---|---|
| Monthly capacity | Committed units per month | Vague ranges |
| Peak capability | Maximum with overtime | Assumes unlimited overtime |
| Current load | Share of capacity used | Refuses to say |
| Seasonal pattern | Busy months | Claims never busy |
| Priority basis | How allocation is decided | No stated rule |
| Subcontracting | Whether and for what | Undisclosed outsourcing |
Subcontracting disclosure
A factory that subcontracts part of your order without saying so has effectively created a vendor you have not qualified. Ask directly and require disclosure.
Sampling a Range With One or Many
Sampling is where the single-versus-multiple decision becomes visible in time and cost.
Where sampling time actually goes
Most sampling delay is approval cycling rather than factory work. Several vendors multiply the cycles, which is why parallel sampling rarely saves as much calendar time as expected.
Batching comments into one consolidated round per vendor recovers much of the difference.
Sampling with one factory
Consolidated sampling is faster to coordinate and produces a coherent set, because the same team interprets every style. The risk is that a weakness in one family goes unchallenged.
Sampling with several
Parallel sampling compresses calendar time but multiplies coordination: several sets of comments, several rounds, several interpretations of the same brief.
Sample the hard styles first
Whatever the structure, sample the most difficult construction first. Discovering a capability gap on the fourth style wastes the time spent on the first three.
Keep range coherence in view
Samples judged individually can look fine while producing an incoherent range. Review them together, in one room, under one light before approving.
Contracts, Tooling and Terms
Structure determines who holds what, and that determines your switching cost.
Documented location
Knowing that you own the tooling is not the same as knowing where it is. A written inventory with photographs and location prevents a slow, expensive search when a switch becomes necessary.
Dies are frequently misfiled, sold with a business, or simply lost between seasons.
Tooling ownership
Where you pay for tooling, you should own it and be able to move it. Tooling held by a single vendor without documentation is a lock-in that surfaces at the worst moment.
Specification and file ownership
Patterns, tech packs and specification files should be yours. A vendor holding the only copy of your construction data has leverage that no contract clause fully offsets.
Terms across vendors
Multiple vendors mean multiple sets of payment terms, lead times and Incoterms. Standardising them where possible reduces the administrative cost that consolidation was supposed to avoid.
Exclusivity questions
A single vendor may ask for exclusivity in exchange for capacity priority. That trade is sometimes reasonable, but it should be priced explicitly rather than granted by default.
| Item | Single vendor | Multiple vendors |
|---|---|---|
| Tooling | One location, easy to track | Document location and ownership each |
| Files | Risk of single copy | Duplicate risk across vendors |
| Payment terms | One negotiation | Standardise where possible |
| Lead times | One schedule | Align shipment windows |
| Exclusivity | Often requested | Rarely necessary |
| Audit rights | One relationship | Apply same clause to all |
Exit provisions
Whatever the structure, the contract should state how it ends: tooling return, file handover and completion of orders in progress. Relationships change; written exits make change affordable.
Moving From Several to Fewer
Consolidation is a migration, not a decision. Handled badly, it transfers volume to a factory that cannot absorb it and loses the quality you already had.
Timing the move
Consolidation is easiest after a season closes and hardest during peak. Attempting a transfer while both factories are loaded invites delay on both sides.
The calendar is part of the plan, not an afterthought.
Start with the family that travels best
Move the simplest, most shared family first. Early wins build confidence and reveal the receiving factory’s real behaviour under new volume.
Transfer style by style, not all at once
Moving an entire family in one order means discovering problems on a full shipment. Moving one style, verifying, then adding the next keeps each risk small.
Keep the losing vendor warm
Until the transition is proven, keep the existing vendor active at reduced volume. Closing a source before the replacement is stable removes your fallback at the moment you most need it.
Re-run sampling, do not assume continuity
A factory new to your style must produce its own approved sample. Assuming a transferred specification will be interpreted identically is the most common consolidation mistake.
| Transition step | Action | Risk if skipped |
|---|---|---|
| Select family | Pick most shareable construction | Complexity on first attempt |
| Resample | New approved sample per style | Different interpretation |
| Pilot order | One style, reduced quantity | Full-shipment failure |
| Verify | Inspection against reference | Checks nothing |
| Expand | Add styles sequentially | Volume overload |
| Retire slowly | Keep old source at lower volume | No fallback |
Watch for the capacity step change
A factory comfortable at two thousand units a month may behave differently at six thousand. Consolidation is also a capacity transfer, and it should be paced accordingly.
Lead Factory Plus Specialists
The two extremes are rarely the answer. Most mature ranges settle into a lead factory carrying the bulk of the work and one or two specialists covering what it cannot.
What the lead factory carries
The lead normally holds the largest family, the shared components and the packaging standard. It becomes the reference for colour, stitch quality and inspection interpretation.
That reference role matters more than the volume share, because it stabilises the whole range.
What the specialists carry
Specialists take the families that need equipment or experience the lead lacks: load-bearing backpacks, insulated pieces, small leather goods with fine edge work.
Giving a specialist a coherent family lets it optimise properly rather than fitting one style into someone else’s process.
Who owns the specification
The lead can hold the master specification even for styles it does not build, provided the specialist agrees to work from it. This keeps terminology and tolerances consistent across the range.
Where that is impractical, the buyer must own the master specification directly, which is the safer arrangement.
Managing the handoffs
The lead-and-specialist model introduces interfaces: shared components, matching colour, coordinated shipment timing. Each interface needs a named owner, or it will be nobody’s job.
| Role | Carries | Typical risk |
|---|---|---|
| Lead factory | Largest family, shared standards | Assumes authority it has not earned |
| Specialist | Family needing specific capability | Works to own interpretation |
| Buyer | Master specification, approvals | Becomes bottleneck if unclear |
| Component supplier | Zips, hardware, lining | Shade drift between batches |
| Inspector | Uniform acceptance decisions | Different standards per site |
Where the Structure Shows Up in Cost
Structure affects cost in places that a quotation does not show, which is why the cheapest quote often belongs to the most expensive structure.
Setup and changeover
Every factory runs setup per style. Consolidating styles into fewer factories reduces the number of setups charged back into the price, though the effect depends on how the factory allocates setup cost.
Material minimums
Each vendor buys material separately, and each purchase carries a minimum. Splitting a range across three vendors can triple the material minimum exposure for the same total volume.
Freight and consolidation
Several vendors mean several shipment windows, several sets of documents and less ability to consolidate containers. The freight penalty is often larger than the price difference buyers negotiate hardest over.
Inspection and administration
Each vendor needs inspection, follow-up, payment processing and reconciliation. These costs are rarely attributed to the structure that created them.
| Cost line | Single factory | Three factories |
|---|---|---|
| Setup per style | Concentrated | Spread and repeated |
| Material minimums | One exposure | Up to triple |
| Freight | Consolidatable | Fragmented |
| Inspection | One protocol | Repeated per site |
| Payment processing | One flow | Multiple flows |
| Problem resolution | One owner | Ownership disputes |
The comparison to make
The right comparison is total landed cost of the range, not unit price per style. Structure-driven costs belong in that total.
Building a Risk Register
Whatever structure you choose, the risks it creates should be written down and owned.
Concentration
Share of volume in any single factory, and what happens to the range if that factory stops for a month.
Capability gaps
Families built by a factory outside its proven competence, and the evidence that supported that decision.
Interface failures
Shared components, colour standards and shipment coordination across vendors, each with a named owner.
Information ownership
Where patterns, specifications and tooling physically sit, and whether you can retrieve them.
| Risk | Likelihood | Response |
|---|---|---|
| Single factory stops | Low but severe | Qualified backup with your specs |
| Capability gap surfaces late | Medium | Sample the hardest style first |
| Colour mismatch across vendors | High | Physical standards, central components |
| Tooling inaccessible | Medium | Written ownership, documented location |
| Peak capacity shortfall | Medium | Written capacity commitments |
| Undisclosed subcontracting | Medium | Contractual disclosure clause |
Review it annually
The register is a living document. Risks change as volume shifts and as factories change ownership, management or product mix.
A Decision Framework
The decision can be reduced to a small number of questions with defined answers.
Question one: how many families?
Count real construction families, not products. One or two favours consolidation; three or more usually favours a split.
Question two: does anyone build all of them repeatedly?
If a factory can show output, equipment and samples across every family you need, consolidation is viable. If not, it is not.
Question three: what is your peak against their capacity?
A peak above one plant’s committed capacity requires a second source regardless of preference.
Question four: how much management capacity do you have?
Multiple vendors consume attention. A very small buying team may reasonably accept weaker fit in one family in exchange for a manageable structure.
The cheapest structure is the one your team can actually run. A theoretically optimal split that nobody has time to manage produces worse outcomes than a simpler arrangement managed properly.
Question five: what is the cost of being wrong?
Where a failure reaches the customer expensively, specialisation matters more. Where the product is simple and forgiving, consolidation risk is smaller.
| Answer pattern | Recommended structure |
|---|---|
| One family, sufficient volume, moderate peak | Single factory with a qualified backup |
| Two families, one dominant | Lead factory plus specialist for the second |
| Three or more families | Split by family, one factory each |
| Any family above one plant’s capacity | Two sources in that family |
| Small team, simple range | Consolidate and accept narrower capability |
| Regulated or technical products | Specialist per regulated family |
Write the decision down
Recording why a structure was chosen, and what would trigger a review, prevents the arrangement from quietly becoming permanent through habit rather than merit.
Revisit the answer annually
Ranges change, factories change and volumes change. A structure that fitted two years ago may now be holding back growth or overloading management.
FAQ
Is one factory always cheaper?
Usually cheaper on administration and modestly cheaper on unit price, but not always cheaper overall. If the single factory cannot build one family well, rework and delay cost more than the administrative saving.
How many factories is too many?
More than your team can review monthly. As a practical guide, three to four vendors is manageable for a small buying team; beyond that, inspection and coordination quality usually decline.
Can a tote factory build backpacks?
It can accept the order, but load-bearing construction requires different reinforcement, machinery and operator experience. Buying a backpack from a tote factory is usually buying a first attempt at your expense.
Should I split one family across two factories?
Generally no, unless capacity requires it. Two factories building the same family doubles interpretation risk and quality variation with no offsetting benefit. Split by family instead.
How do I keep quality consistent across vendors?
One written specification, one signed reference sample per style held by each vendor, one inspection protocol with calibrated inspectors, and centrally nominated shared components such as zips and hardware.
What if my volumes are too small for several factories?
Then consolidate and accept narrower capability, or reduce the number of families in the range. Spreading small volumes across many vendors produces poor pricing and little leverage anywhere.
How do I protect myself with a single vendor?
Own the tooling and files, keep a qualified backup that has passed sampling, retain reference samples, and benchmark pricing periodically against the market rather than against last year.
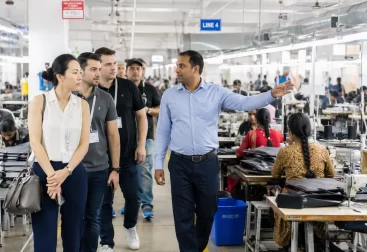
Do I need a factory visit to judge capability?
A visit helps, but equipment inventory, production mix and the hardest available sample usually answer the capability question faster. A visit confirms what the documents suggest.
How long does consolidation take?
For a simple family, one sampling round plus a pilot order. For a complex family, two to three sampling rounds and a full season before the original source can safely be retired.
What is the biggest mistake buyers make here?
Consolidating to reduce administrative work without checking that the receiving factory builds that family repeatedly. The saving is immediate and the quality cost arrives a season later.
Should the same factory handle packaging and labelling for all styles?
Where possible, yes. Packaging consistency across a range is easier to control from one point, and carton specifications affect freight calculations across the whole order.
How many construction families does a typical range contain?
Most mid-sized bag ranges contain two or three real families once grouped by construction rather than by product name. That count, not the number of styles, drives the sourcing decision.
Planning a range and unsure whether to consolidate or split?
Send your style list and target volumes to info@gionar.com and we will help you group the range into production families and identify where a single partner can carry the work.